


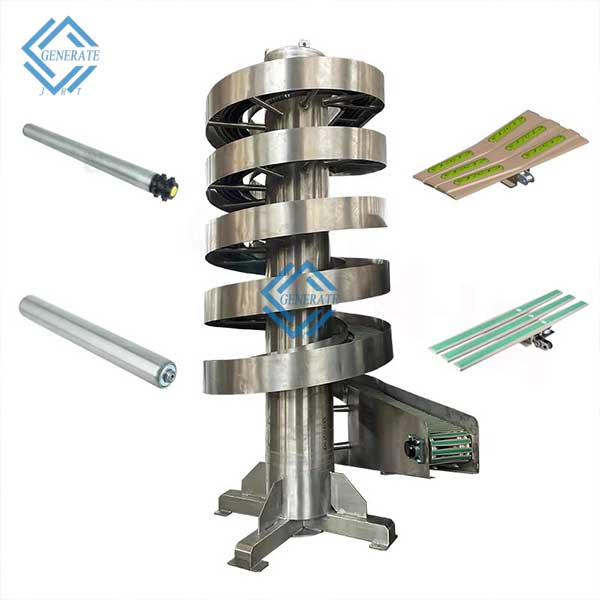


Vertical Rolling Conveyor Systems: The Ultimate Space-Saving Solution
Tired of inefficient floor plans and long, space-consuming inclined conveyors? Our state-of-the-art Vertical Rolling Conveyor systems are engineered to optimize your facility's layout by moving products vertically with maximum reliability and a minimal footprint. Designed for seamless integration into production, packaging, and distribution lines, our conveyors provide the critical vertical elevation change you need to maximize space and boost productivity.
What is a Vertical Rolling Conveyor?
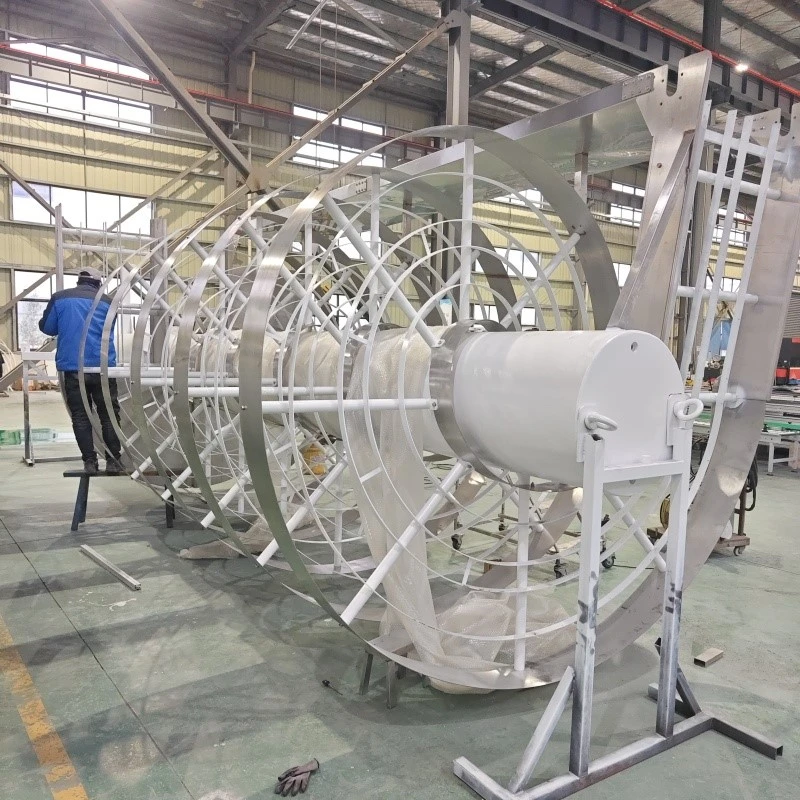
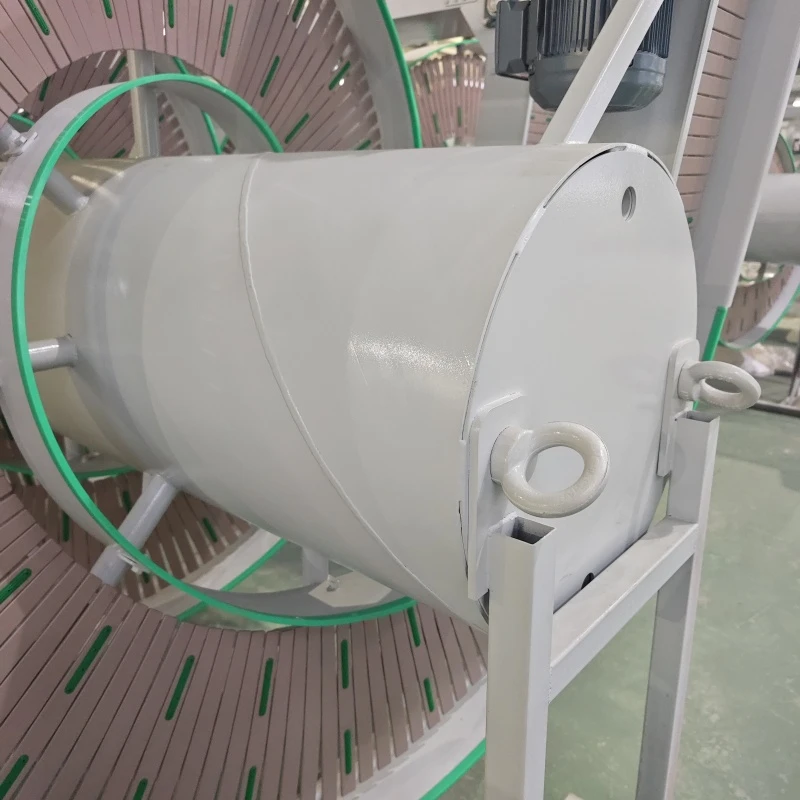
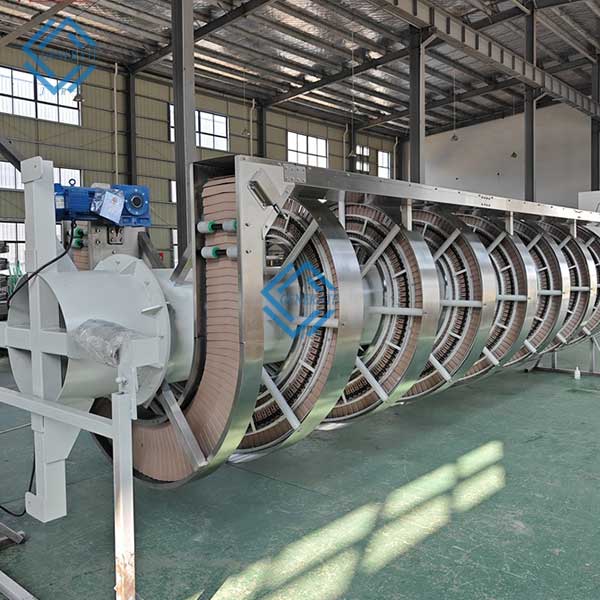
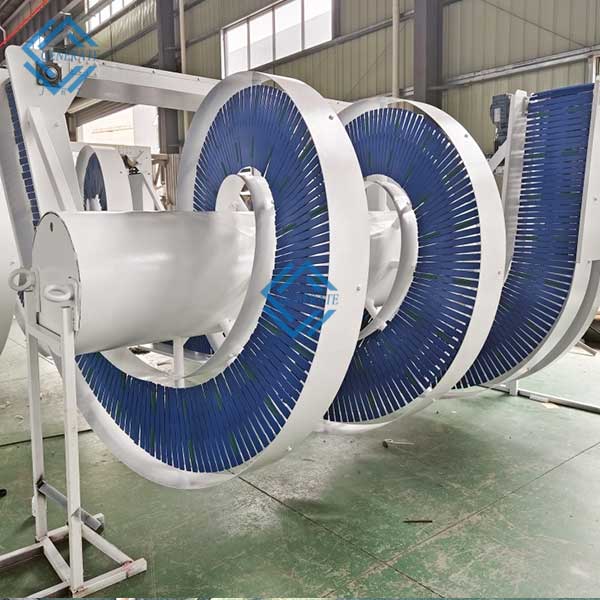
A Vertical Rolling Conveyor is a continuous lifting system designed to transport goods-including boxes, totes, bags, and packaged products-directly between different elevations. Unlike sloped conveyors, our systems move materials straight up or down, saving invaluable floor space. Products are securely loaded, gently stabilized on a rolling carrier, and transported vertically before being discharged smoothly onto the outgoing conveyor line. This makes them the ideal conveyor for multi-level facilities and high-density warehouses.
Key Features & Benefits (Keyword-Rich Bullet Points)
Maximize Floor Space: Eliminate long, inefficient ramp conveyors. Achieve a significant vertical lift in a compact footprint, freeing up space for other operations.
Gentle & Secure Product Handling: Our proprietary carrier and guiding system ensures products remain stable and prevent damage during ascent and descent. This is essential for fragile or high-value items.
High Throughput & Efficiency: Engineered for continuous operation, our vertical conveyors keep your lines moving 24/7, seamlessly integrating with automated systems to handle high volumes.
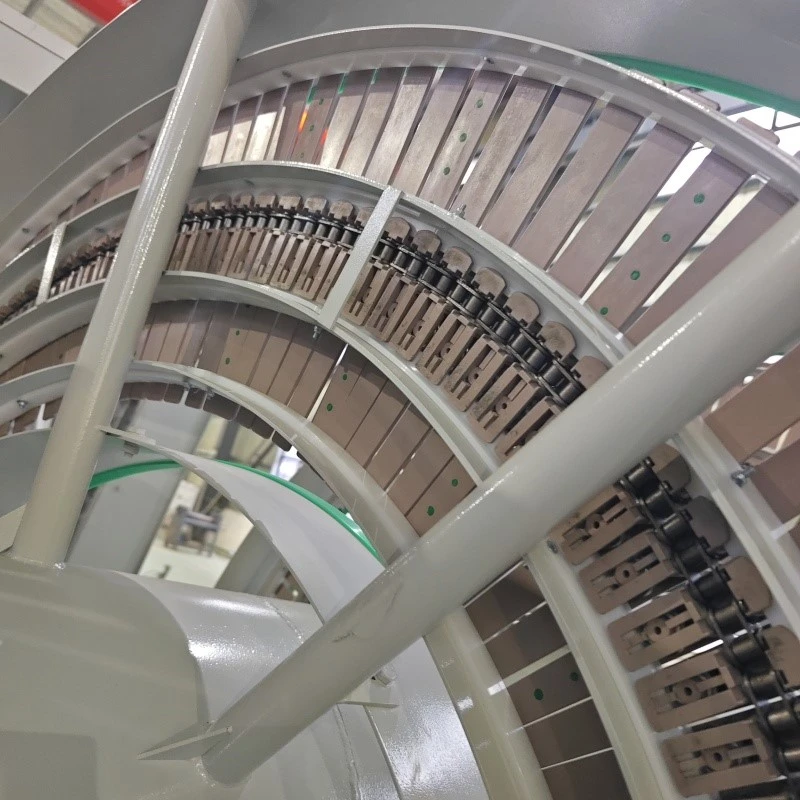
Robust & Durable Construction: Built with high-grade materials, dual chains, and precision guide rails for low maintenance and long-term reliability in demanding industrial environments.
Customizable Solutions: We offer tailored designs with adjustable widths, heights, speeds, and carrier types to meet your specific application needs, whether for manufacturing, food processing, or logistics.
Improved Safety: Enclosed design with integrated safety guards and interlock systems protects operators and ensures compliant operation.

Technical Specifications (Keyword: Vertical conveyor specifications)
| Feature | Description |
|---|---|
| Common Applications | Boxes, Totes, Cartons, Bags, Packaged Goods, Parcels |
| Standard Load Capacity | Up to 100 lbs (45 kg) per carrier (custom capacities available) |
| Lifting Heights | Customizable from 10 feet to over 50 feet (3m to 15m+) |
| Speed & Throughput | Configurable speeds; typically 30+ units per minute |
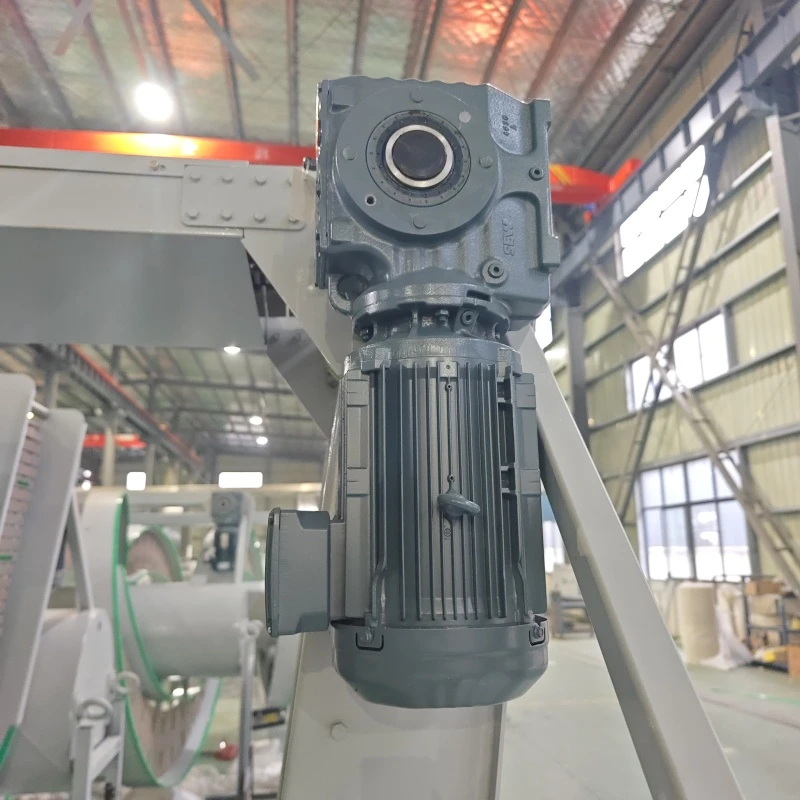
| Drive Options | Top-mounted electric motor with gear reducer |
| Frame Material | Powder-coated carbon steel or stainless steel (USDA approved) |
| Control Integration | PLC compatible with standard interfaces for easy line integration |

Industries & Applications
Our vertical conveyors are versatile solutions for a wide range of sectors:
Warehousing & Distribution (Logistics): Perfect for multi-level order fulfillment centers and automated storage and retrieval systems (AS/RS).
Food & Beverage: USDA-approved stainless steel models available for vertical transport in food processing and packaging plants.
E-commerce & Parcel Handling: Efficiently move parcels and packages between sortation levels.
Manufacturing & Production: Integrate into assembly lines to feed parts or finished products to different floor levels.
Pharmaceutical & Consumer Goods: Handle totes and boxes gently in clean, high-value environments.

Why Choose Our Vertical Rolling Conveyor?
At Zhengzhou Generate Machinery Co., Ltd. , we don't just sell conveyors; we provide material handling solutions. Our team of experts works with you from design to installation, ensuring a system that perfectly fits your workflow. With a focus on quality, reliability, and innovative engineering, our conveyors are built to perform day in and day out, reducing your operational costs and increasing your ROI.